Solutions for
RTU cartridges or syringes
RTU manufacturing carries more value - and more responsibility.
Ready-to-use manufacturers are taking on a critical role in biopharmaceutical supply chains. By supplying cartridges or syringes already washed, depyrogenated, siliconized, assembled, packaged and sterile, they enable pharma companies to outsource container preparation and the associated validation burden.
With the injectable-drug market projected to expand 1.9×, rising volumes intensify the challenge: RTU manufacturers are therefore carrying more value and more responsibility providing complete documentation for customer qualification.
3
functional attributes preserved: container-closure integrity, break-loose and glide performance, while particulate levels were not adversely affected by the steam-sterilization process
0
adverse shift in the mean values or distribution of break-loose and glide forces, confirming preserved baked-on siliconization functionality
0
particulate increase detected: no increase in fibres or particles generated by the Tyvek® lid or packaging after moist-heat sterilization
0
CCI failures confirming that the thermal process preserved closure performance
SELECTING THE APPROPRIATE STERILIZATION METHOD IS ONLY THE BEGINNING
An RTU manufacturer must demonstrate sterility while preserving every attribute required for customer qualification and release.
From closure integrity and gliding performance to particulate control, seal strength, printing and dryness.
Our capabilities on RTU cartridges and syringes demonstrated the required sterility without adversely affecting container-closure integrity, break-loose and glide performance or particulate levels. The results confirmed that closure functionality and baked-on siliconization remained intact, with no increase in fibres generated by the Tyvek® lid or packaging.
The outcome is a customer-ready RTU system, backed by documented evidence and proven for repeatable industrial-scale production.
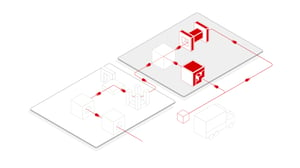
saturated-steam cycles are developed around the complete cartridge, nest, tub and sterile-barrier configuration
H₂O₂ treats thermosensitive configurations through controlled vacuum, vapour delivery, temperature management and aeration, according to material compatibility and packaging permeability.

emerge sterile, dry and ready for immediate use.
Can experience with prefillable syringes support RTU cartridge development?
Yes. Both families present siliconized glass surfaces, assembled components, nested packaging and pressure-sensitive sterile barriers. This experience strengthens process understanding, but each cartridge configuration remains independently developed and validated because its geometry, components and load arrangement are specific.
How can sterilization capacity grow with RTU volumes?
Capacity is engineered across the complete system. Automated transfer reduces handling time, while upstream preheating or conditioning and validated downstream drying, conditioning or aeration release the main chamber earlier. This increases effective output without relying only on a larger sterilizer.
How does the machine prevent condensation during the cycle?
The equipment controls chamber and load temperature throughout conditioning, injection and exposure. Maintaining the required temperature margin supports homogeneous vapour distribution and prevents condensation that could compromise penetration, material compatibility or residual removal.
Why must the process be developed around the complete RTU system?
The sterilant does not interact with the cartridge alone. Nest density, tub geometry, porous lids, protective bags and load arrangement influence air removal or vapour access, exposure, condensate formation, drying and aeration. The complete configuration must therefore be treated as one defined load.
Which sterilization process can be used for RTU cartridges?
Saturated steam is selected when the complete cartridge and packaging configuration tolerates heat and moisture. Low-temperature H₂O₂ is selected for thermosensitive configurations with compatible materials and permeable sterile-barrier packaging. The two routes are not automatically interchangeable: the complete commercial system must be tested and validated.
Can sterilization affect cartridge functionality?
An unsuitable process can affect packaging, assembled components or siliconized surfaces. Development must demonstrate microbial effectiveness together with preservation of the relevant functional attributes. Sterility is not sufficient if the cartridge no longer performs as specified during filling or administration.